
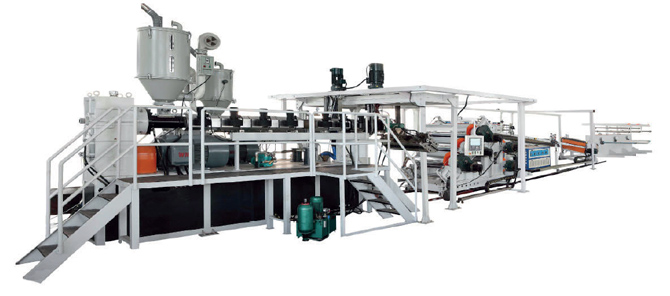
Sheet extrusion with raw material pet and pet on the agenda
Yavuz Eroğlu-pagev 1. Vice President, SEM plastic general manager
Yavuz Eroğlu-pagev 1. Vice President, SEM plastic general manager
Among the raw materials used in the plastic packaging sector, especially pet and PP are replaced by PVC and PS very quickly. Especially PP and pet will be the most basic raw materials of the future. Although PP is our favorite (yet flexible module value (Flexural Modulus) and can not capture pet in transparency) , pet's PVC ‘in the world for processing this raw material due to the stunning fast and clear reason , many investments have been made in our country and more. Pet textile and packaging industry has become a very important raw material. According to our analysis only ,pet plate extrusion capacity in plastic packaging sector has reached 50,000 tons / year in 17 companies .
Especially in the plastic packaging and textile sector, SEM invested in sheet extrusion in 2007. Since then , we have accumulated a considerable knowledge about the problems and solutions experienced in the process of gaining experience in our company and in our meetings with our technical staff and in our literature researches. Packaging industry , especially for injection machines and PS , PP, PE raw materials in many “ Problem - Solution “ format brochures , booklets, etc. these types of sources are very limited when present, especially for pet sheets. I would like to present this study on “ basic problems and solutions in pet sheet extrusion“, which was compiled from the experience of our technical department, in order to be an entry point for the studies to be carried out in order to fill such a gap and to share the practical information of our company which is producing such a production with Since all the problems experienced will exceed the size and purpose of this study , only the most basic and frequently encountered problems and their solutions have been discussed in this article.
The purpose of this technical introduction is to enlighten those who want to produce Apet sheets by processing pet on plate lines.It should be dried for 6 hours before the PET production. ( Conventional method , new systems based on Infrared in the market claims to shorten this time.) Drying pet is the most important point of the process. This topic alone is sensitive enough to be detailed with a special article.
Dryer: humidity-40C, and at least 1 kg/hour for pet 1.5 M3/minute air-driven moisture-absorbing type dryer is required.
Extruder : L/D ratio ( the ratio of the length of the screw to its diameter) is between 28 and 32 and the compression ratio is between 2.5 and 3 , an extruder is suitable for this work. A barrier Type Screw is best suited for this task , because it gives better melt and capacity. In the researches and experiments, higher capacities were obtained in the lower screw speed (rpm) of pet compared to other raw materials. As a matter of fact, it is important that the main engine and driver mechanism produce good torque at low screw speeds.The heat settings are determined according to the screw diameter and other factors. The following is an example from the point of view of giving an opinion.
Regions K1 K2 K3 K4 K5 FD KF1 KF2 KF3
Temperature ° C 290 290 285 285 280 280 275 275
Note: K1 ~ K5 are bucket temperatures, (K1: feed zone raw material entry), FD zone is filter replacement zone and KF1 ~ KF3 is extrusion head (mold) zone.
The feeding zone should be cooled well so that the goods are not wrapped and the extruder can be fed regularly.
Head ( mould ) : play lips , suspension type head is required. The distance between the head and the Kalender should be minimum to prevent sagging ,since the molten resistance of the pet is very low. (60 mm or less) . That's why the pet heads are crooked. Side-limiting metal plates (plate width adjustment bars) for adjusting the width of the plate should not be outside the head. Because in such heads, when the pet flows inside, it creates certain blind spots and the pet can break down here.
Kalender : according to the thickness of the plate to be produced , Kalender can be vertical/horizontal/inclined. Our advice is to make a decision according to the thickness of the thickness of the horizontal or inclined type kalenderlar.Cylinder temperatures vary according to diameter and water channels inside. Temperatures should be around 45. The temperature of each cylinder can be kept between 20 C and 60 C with the help of a thermoregulator. Gear-controlled cylinders give smooth , uncoated sheets according to those moved by chains.Independently controlled servomotor cylinders should be preferred.
Other equipment : corona application ( to reduce static electricity load) , prevents dust during sheet drawing and winding. In addition ,silicone pools prevent pet plates from sticking together and clogging. (The sheet is available in the market in the form of a separate granule which prevents the plate from sticking and blocking.)
Side Wasteler : side wasteler not exceeding 2% - 3% of total sheet weight can be fed directly from the dryer by mixing with the original pet. However, this is a delicate process, the process must be done quickly with a smooth and good breaking machine. ( the thickness of the slab , the rate of the side furnace and the rate of the crushing machine's powder making are important parameters.
PROBLEMS AND SOLUTIONS :
Problem : dark lines or dots , Darkening of the plate (darkening of the plate))
Possible Causes Of This Problem :
1 - pet decay due to excessive temperature during processing. This can be caused by high hive temperatures , the rotation of the screw, and the friction of the material.
* if the lips of your head are not cleaned well , parts of the lip may be stuck. These particles can break down over time and make a mark.
* The holes in Vida , The Hive or the head can cause the goods to get stuck here and deteriorate over time.
* If the screw is too long between the pins , the return speed of the Screw should be increased.This prevents the goods from escaping back or warming up too much. Because if they are long between the Burgundy, the goods are too hot.This problem is solved by turning the screw fast.
2) the dirt coming from the environment,dust or dirt coming without breaking,dust or the dust previously left in the dryer , dust can be.
Solution:
Reduce the hive temperatures, clean the environment or change the design of the screw and provide a more comfortable flow.
Problem : a plate surface similar to the peel of an orange.
1) reasons for this problem
The surface of the plate is torn while leaving the head. This is because the surface of the head is not very bright(slippery).
Solution: increase the temperature of your head or melt so that the product flows more smoothly.
2) the probable cause of this problem :
Irregular drawing of plate surface during cooling (shrinking)
Solution: raise Kalender temperatures.
Problem : there are holes on the plate.
1) the probable cause of this problem :
There is moisture in the slab.
Solution: dry the raw material better.
2) the probable cause of this problem :
There are air bubbles in the slab.
Solution: gradually raise the temperature of the hive areas to be considered close to the funnel . So you can throw the air back out of the funnel. Increase the pressure at the inlet of the gear pump.
3) the probable cause of this problem :
Steam or gas is formed due to the failure of the set.
Solution: dry the raw material well. Check that the extruder is too hot and not roasted. Lower the Hive heat. Lower the extrusion speed.
PRB : surface plate with fog
1) the probable cause of this problem :
Crystallization occurs due to hot calender cylinders, or a very large lip is made in the calender cylinder or extrusion process is very slow ( especially at the calender speed).
Solution: lower the temperature of the Kalender rollers. Reduce (or eliminate) the lip in front of the cylinder, increase the extrusion speed(especially the calender speed).
2) the probable cause of this problem
An inappropriate material is mixed into the raw material , for example a slider powder, any foreign substance, etc.
Solution : clean the foreign substance from the raw material.
PRB : surface rough
1) the probable cause of this problem
Humidity
Solution : dry the raw material very well.
2) the probable cause of this problem :
There's air between the slab.
Solution : Move the head closer to the Kalender roller or try to make the head and roller more vertical.
3) the probable cause of this problem :
The plate parts from less Ware are not ironed by the Kalender cylinder.
Solution : cut the screws from the plate parts of the goods and increase the ones from the less.
4) probable cause of this problem :
Even very small cracks on very hot Kalender rollers pass to the surface of the sheet.
Solution: lower the calender roller heat .
5) probable cause of this problem
From the calender cylinders , there is a sign on the plate.
Solution : clean the rollers very well.
6) probable cause of this problem :
Kalender is not very bright.
Solution : adjust the gap between the cylinder and the cylinder well . send the rollers to polish.
Problem : the plate consists of lines toward the direction of the machine.
1) the probable cause of this problem :
On the lips of your head , particle , scratches , burns, etc. are available.
Solution : clear the head.
2) the probable cause of this problem :
There are scratches on the Kalender roller.
Solution : rock and polish the surface of the cylinder Kalender.
3) the probable cause of this problem :
Rubber cylinders that pull the plate may be circled and drawing the plate.
Solution : correct the pulling side of the plate.
After all this general preliminary information , our expectation is that our country , especially in Western countries, uses the Turkish Industry's advantage in adapting to new technologies, as well as many disadvantages of late industrialization.